Hairise Provides Modular Belt, Slat Conveyor Chain And Automatic Conveyor System Solutions Since 2004.
Language
Hairise Provides Modular Belt, Slat Conveyor Chain And Automatic Conveyor System Solutions Since 2004.
In order to meet the increasing demands for automation, efficiency, & hygiene, the food sector has consistently been at the forefront of using modern technology. Modular belt conveyors are among these cutting-edge innovations which have revolutionized the way food is grown, packaged, & delivered. These advanced innovations are now essential for survival in today's day in a business with strict regulatory standards.
Manufacturers are under immense strain to improve their processes as customers want food products that are safer, fresher, as well as more sustainable. In addition to meeting these requirements, modular conveyor system offer an unparalleled degree of scalability, durability, & flexibility. They help with many facets of food production, from minimizing the risk of contamination to improving workflow efficiency, consequently their function goes beyond basic transportation. These conveyors have served as the foundation of a quickly changing food manufacturing environment through the use of cutting-edge technology & upholding stringent hygiene requirements.
The innovative layout of modular belt conveyor systems relies on its interconnecting thermoplastic modules, which have been reinforced for remarkable longevity. These modular structures, in contrast with traditional conveyor systems, allow for them to be easily expanded, contracted, or changed without needing a whole system redesign. Businesses may adapt to shifting demands for production due to this flexibility without experiencing long periods of downtime.
The food sector places a high priority on sanitation, therefore modular conveyors have been developed to satisfy the strictest sanitary requirements. Their surfaces are clear of crevices, which prevents germs from growing, which has become an important challenge in conventional conveyor systems. Furthermore, the materials used for producing these conveyors meet FDA & USDA food-grade standards, assuring food safety through the whole production process.
In addition, modular conveyor system offer an extensive selection of functions that may be modified to meet a variety of food processing needs. These systems may be utilized for a variety of tasks, including moving larger things like frozen meats or delicate baked products, because of the built-in cleats, side guards, & perforations. Across many manufacturing lines, this level of customization guarantees peak efficiency and effectiveness.
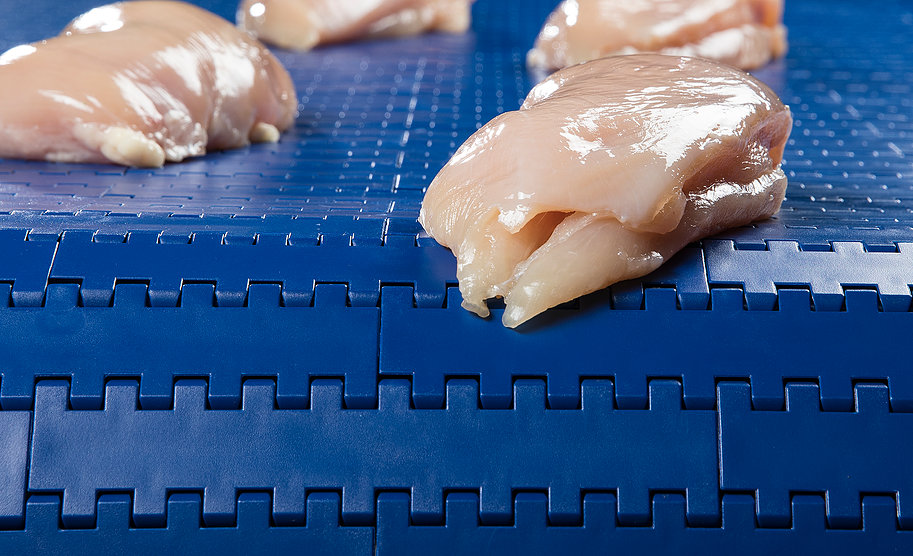
In addition to gaps and seams in the cloth, traditional conveyor systems were susceptible to microbiological contamination, making complete cleaning challenging. Due to their impermeable surfaces and simple disassembly, modular conveyor systems address this problem & enable rapid and efficient sanitation without the need for specialized machinery. As an instance, by using modular solutions, meat packing operations have significantly reduced downtime during cleaning processes while preserving adherence to strict hygiene regulations.
Another area in which modular chain conveyors are good is efficiency. Modular belt conveyor design enables it to move between product lines faster, for example, from frozen items to baked products. These are also important in contemporary food processing facilities because of their adaptability in handling an extensive variety of product types, from hefty meats that have been frozen to delicate pastries.
In the food sector, safety is an essential concern. Modular conveyors resolve this issue through offering slip-resistant surfaces which ensure the safe transportation of wet or delicate food items. Furthermore, these systems meet with international safety standards, giving consumers & producers piece of mind.
The severe conditions frequently observed in food processing have been created to be handled by modular belt conveyor systems. They are resilient to harsh cleaning solutions & show tolerance to high temperatures, either in freezing or baking conditions. Relative to conventional systems, the system's durability guarantees a longer lifespan, lowering the demand for frequent replacements.
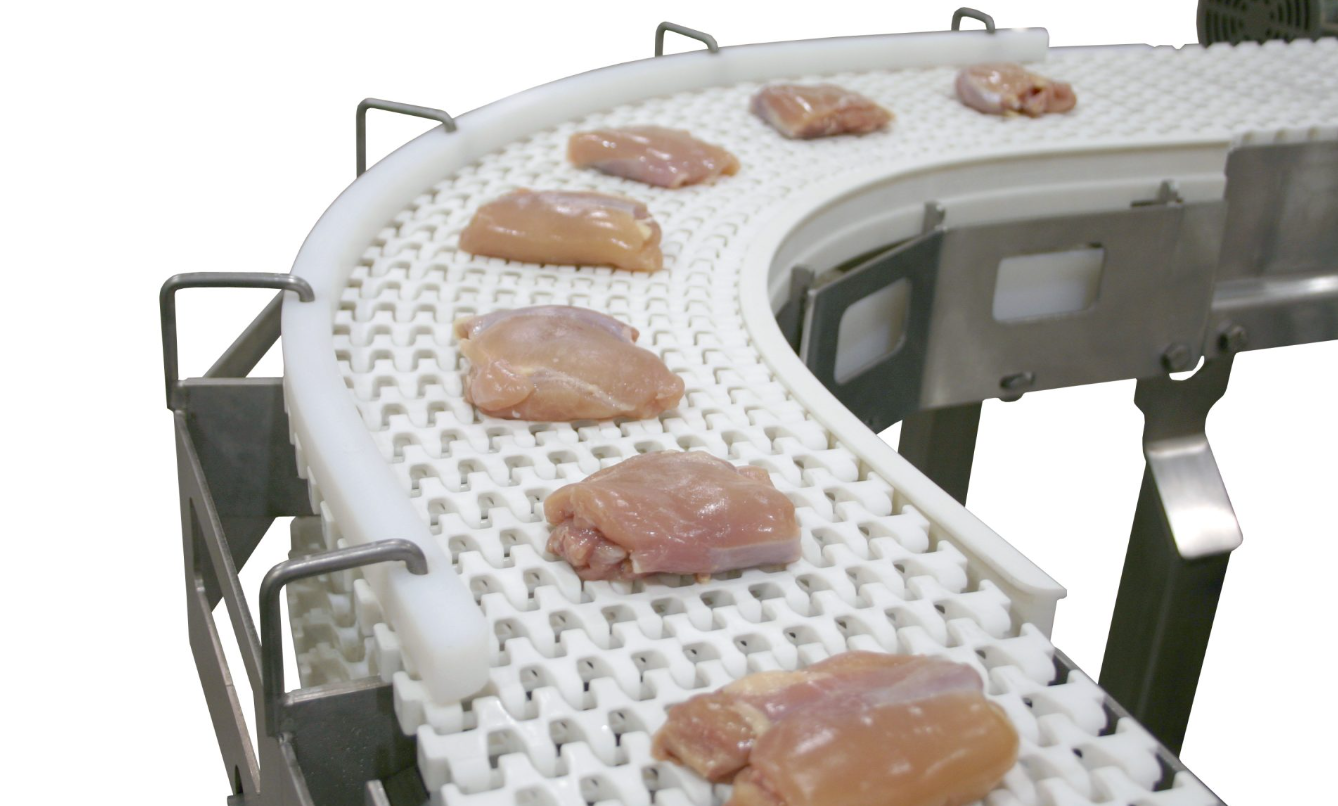
Modular belt conveyors serve as crucial to decreasing contamination risks in the processing of poultry and meat. In order to provide frequent exposure to raw and processed goods without compromising cleanliness, these systems have been designed to transport entire carcasses or ground beef.
When handling delicate products like yogurt and cheese, smooth modular surfaces are best since they reduce product damage. As an instance, dairy processing facilities utilize modular systems to move containers of milk with smooth alignment, improving efficiency in the workflow.
Modular belt conveyors are extremely useful to the baking & confectionery industry, particularly in conditions with temperature swings. By efficiently moving goods between proofing ovens to cooling stations, these structures reduce product damage during transportation. One notable case study is on a large bakery which utilized modular conveyor system to reduce down on product damage by 20%.
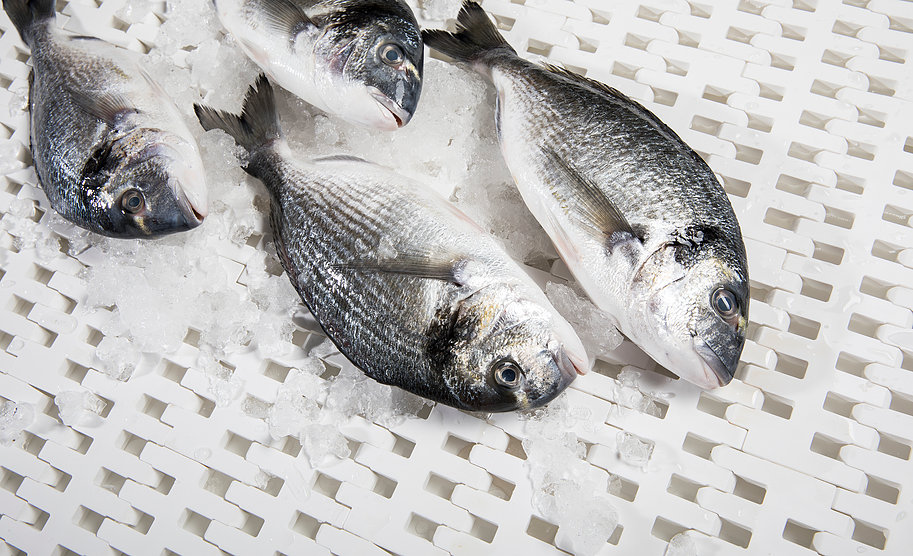
Equipment that can deal with delicate items and resist seawater is necessary for seafood processing. Due to their ability to resist corrosion, modular belts are perfect for cleaning and moving both fresh and frozen seafood in the supply chain.
The affordability of modular chain conveyors constitutes one of its main benefits. Maintenance costs are substantially reduced by the straightforward substitution of defective modules. As an example, it has been demonstrated that modular systems have a 30% longer lifespan than conventional ones, this saves manufacturers money over time.
The effective operation of modular belt conveyor system is further enhanced by integration with modern technologies like sensors and artificial intelligence. These equipment simplify fruit, vegetable, & grain classification and sorting lines by enabling continuous monitoring & automatic changes.
Modular conveyors utilize recyclable materials in its construction to meet the food industry's increasing worries about sustainability. They additionally reduce food waste & product spills throughout transportation, which falls in line with the industry’s push toward ecology friendly practices.
Even while modular belt conveyors cost greater up front, they are considerably more advantageous in the long run. As time passes, a strong return on investment is guaranteed by less downtime & increased operating efficiency.
Workers might find the shift to modular systems challenging. On-site repair and maintenance training programs, however, may effectively address this issue and guarantee smooth incorporation into present operations.
IoT-enabled innovative approaches are the way of tomorrow for modular conveyor system. By tracking belt wear, speed, & product weight instantaneously, these advanced technologies reduce unscheduled downtime & allow predictive maintenance.
Manufacturers are developing bio-based polymers for food-grade modular belts as sustainability gains traction. The adverse environmental impact of these systems is also being mitigated by the growing use of carbon-negative manufacturing techniques.
Modular chain conveyors are being transformed by AI integration, making it possible to make intelligent decisions whereas sorting food. AI-powered devices, for example, may detect foreign items or harmed products in the course of transportation, ensuring the security and efficacy of the product.
In the food sector, modular belt conveyor systems have transformed efficiency, safety, & cleanliness, rendering them essential equipment for modern food processing. They have the potential to have a major impact in the foreseeable future of food processing due to their capacity to tackle the primary problems facing the sector, including increasing workflow efficiency and improving sanitary conditions.
Going forward, the opportunities of modular belt systems will be enhanced further by continuing incorporation of sustainable practices & smart technology. In addition to future-proofing their operations, companies who make investments in these innovative solutions now are also helping to create a more environmentally friendly and efficient food supply chain. Modular belt conveyors are the cornerstone of advancement in an industry fueled by innovation and its customer needs, ensuring the food industry's continued resilience, adaptability, as well as competitiveness. Find out more about Hairise modular belt!
LEAVE A MESSAGE
As a automation Conveyors Manufacturer, Plus Modular Belts and Components, Hairise is your right reliable and winning choice.
As a plastic conveyor belt manufacturer & modular conveyor belt supplier, Hairise is your right reliable and winning choice.